Definitions related to calibration requirements and metrological traceability.
In this entry we talk about some definitions related to metrological traceability and calibration requirements.
Specifically, we will discuss, among others, the concepts of traceability, calibration chain, repeatability and reproducibility. We will also indicate meanings related to the measurement, such as measurement, results, accuracy, precision, errors and uncertainty of the measurement or tolerance interval. Likewise, we will address concepts related to calibration, such as metrological verification, calibration intervals, calibration program or certificate.
Metrological traceability
Metrological traceability
We can define metrological traceability as the property of a measurement result by which the result can be related to a reference by an unbroken and documented chain of calibrations, each of which contributes to the measurement uncertainty.
Thus, metrological traceability is an essential property of any measurement carried out in a testing and calibration laboratory.
Now, this is not the only area for which metrological traceability in measurements is essential. Thus, it is also the case in inspection entities (regulatory or not); for reference materials suppliers; or by providing a reference value in a proficiency test. The same thing happens in the context of a product certification; in a commercial transaction; or in the exercise of the functions of public powers. Likewise, it is essential in the control of production processes; and in the acceptance of products, or to decide on their free circulation. Finally, it is also an essential property of any measurement in a laboratory or inspection, development, or design department, or in a technical office.
Thus, if metrological traceability is a requirement, the measuring equipment must be calibrated and/or verified. This must be done at specified intervals, or before use, against measurement standards traceable to international or national measurement standards.
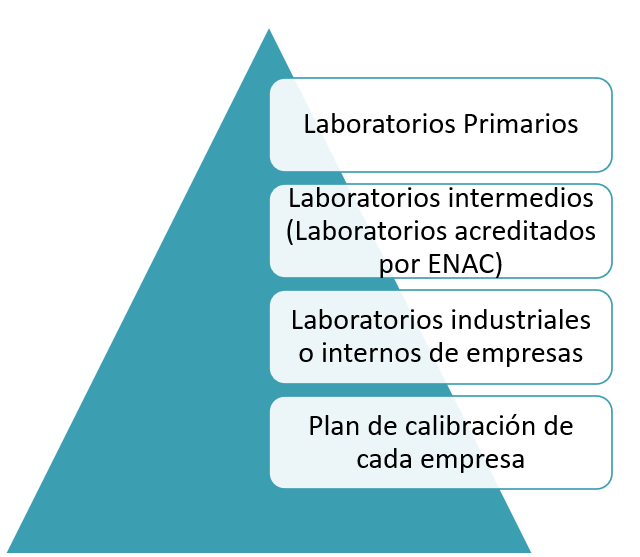
It must be taken into account that sometimes the abbreviated term is simply used 'traceability' so much to talk about 'metrological traceability', as for other concepts such as traceability of a sample, a document, an instrument, a material, etc. It is therefore preferable to use the full form of the term, that is, 'metrological traceability', to avoid confusion.
Calibration Chain
The calibration chain, or chain of connection to standards, is the unbroken chain of comparisons.
The connection with the patterns is the way in which the link with these standards is made.
Definitions related to the measurement process
Measurement
Measuring consists of experimentally obtaining values that can reasonably be attributed to a magnitude. This involves a comparison, usually with a conventional value.
Measurements must be carried out in such a way that:
- Metrological traceability to (inter)national standards is ensured.
- The uncertainty of the measurements made is determined.
Size
Measurement is the action of quantitatively determining the magnitude, size or quantity of something, using specific units to express the result.
Measurement results
Measurement results are the numerical values or data obtained through the measurement process.
These results are subject to errors and the precision of the instrument used.
Boss
A standard is an element with specific properties and precise dimensions that is used as a model or reference for calibration and validation of measurements.
A standard is usually used as a reference to obtain measured values and associated measurement uncertainties for other quantities of the same nature, thus establishing metrological traceability, through calibration of other standards, instruments or measurement systems.

Reference material
The realization of the definition of a given quantity can be established by a measurement system, a materialized measurement or a reference material.
It is a material with well-known and certified physical, chemical or biological properties. This allows it to be used as a reference for calibration and validation of measurements.
Measurement accuracy
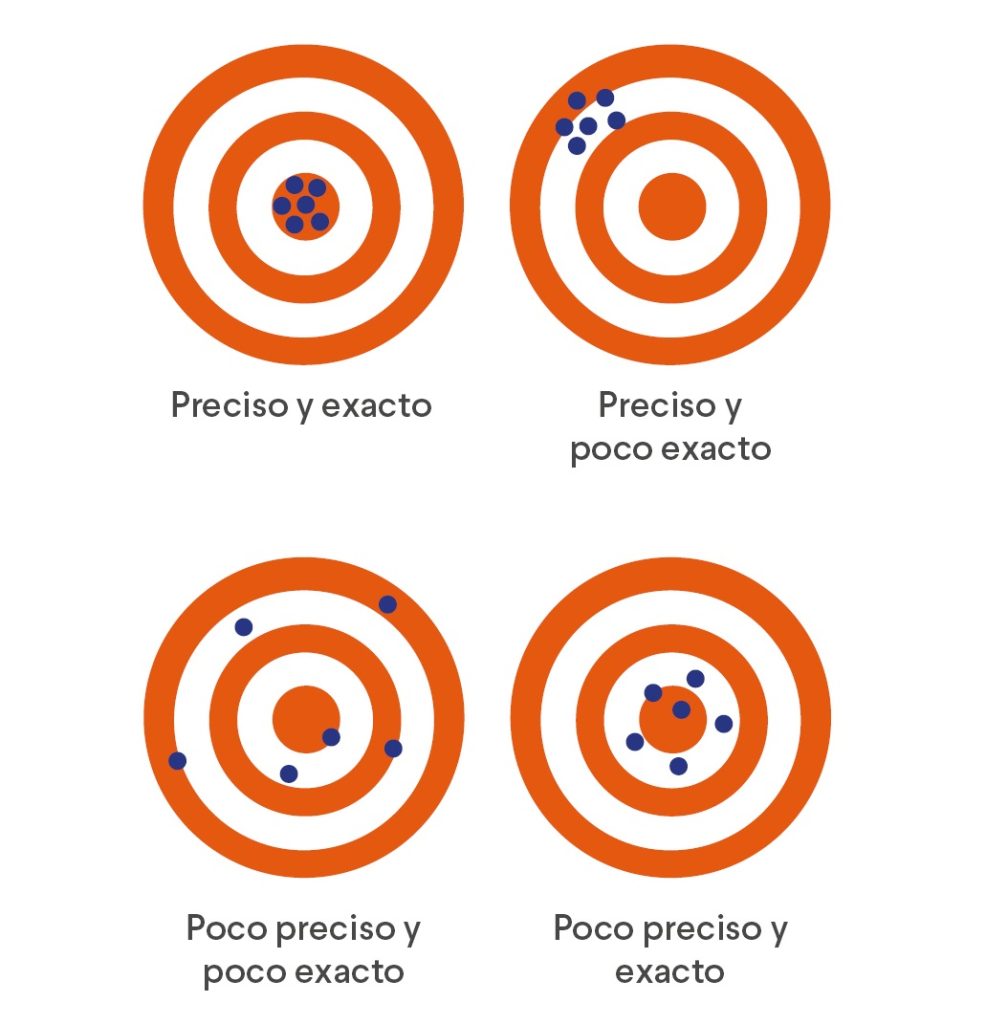
Measurement accuracy is the proximity between a measured value and a true value of a measurand.
The term 'accuracy of measurement' includes the terms 'precision of measurement' and 'veracity of measurement'; so 'accuracy of measurement' should not be used in place of the other two terms.
measurement accuracy
It is the proximity between indications or measured values obtained in repeated measurements of the same object, or similar objects, under specified conditions.
It is common for the precision of a measurement to be expressed numerically by measures of dispersion such as the standard deviation, variance, or coefficient of variation under specified conditions.
The conditions specified may be repeatability conditions, intermediate precision conditions, or reproducibility conditions.
Precision is used to define measurement repeatability, intermediate precision, and reproducibility.
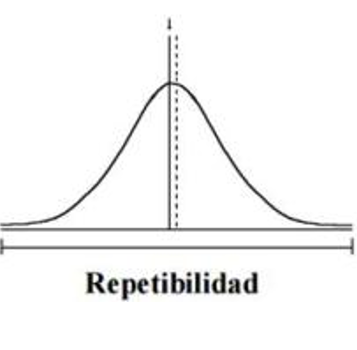
repeatability
The repeatability condition of a measurement is the measurement condition, within a set of conditions that includes the same measurement procedure, the same operators, the same measurement system, the same conditions and operation and the same place, as well as measurements repeated repetitions of the same or a similar object in a short period of time.
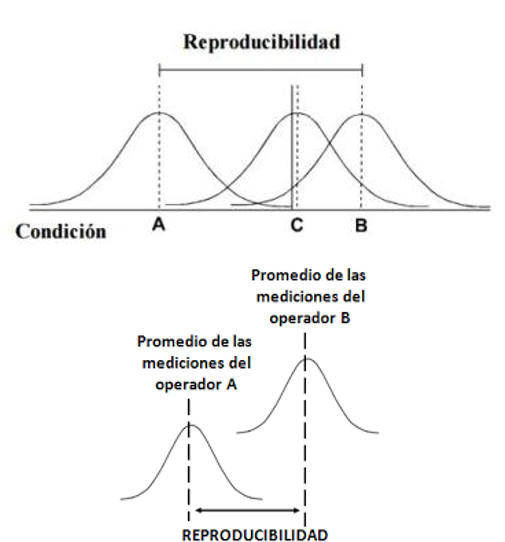
Reproducibility
The reproducibility condition of a measurement is the measurement condition, within a set of conditions that includes different locations, operators, measurement systems and repeated measurements of the same or similar objects.
That is, measurement reproducibility is the measurement precision under a set of repeatability conditions.
Litigation, Arbitration
Measurement results have variability due to multiple causes and this variability contributes to uncertainty. Instrument resolution also contributes to this uncertainty. The interactions between variability and resolution are complex and it is usually chosen to add them.
The variability of the measurement process depends on many causes, many of them external to the instrument:
- Magnitude of influence
- Characteristics of the measurand
- Operator Features
Therefore, its determination corresponds to the user and not to the calibration laboratory. However, the variability during calibration will usually be less than that measured during use of the instrument.
Thus, the laboratory can give a minimum limit for the variability during the measurement based on its knowledge of the variability during calibration.
Measurement errors
Measurement error is the difference between a measured value of a magnitude and a reference value.
This concept can be used in the following cases:
- When there is a single reference value, as in the case of performing a calibration using a standard whose measured value has a negligible measurement uncertainty, or when a conventional value is taken, in which case the error is known.
- When the measurand is assumed to be represented by a single true value or by a set of true values, of negligible amplitude, in which case the error is unknown.
Measurement uncertainty
The quality parameters of a measurement process are its metrological traceability and uncertainty.
The uncertainty is estimated from the different elementary uncertainties linked to the measurement considered, among which is the uncertainty about the knowledge of the reference used during the comparison.
Thus, there is no metrological traceability without uncertainty, nor uncertainty without metrological traceability.
Tolerance range
Every requirement on a physical quantity falls within a tolerance interval (specified tolerance). This is a range of values that is established to determine the acceptability of a measurement.
Definitions related to calibration
Calibration
A calibration is an operation that under specified conditions establishes, in a first stage, a relationship between the values and their associated measurement uncertainties obtained from the measurement standards, and the corresponding indications with their associated uncertainties and, in a second stage , uses this information to establish a relationship that allows obtaining a measurement result from an indication.
Thus, a calibration can be expressed by a statement, a calibration function, a calibration diagram, a calibration curve or a calibration table. Furthermore, in some cases it may consist of an additive or multiplicative correction of the indication with its corresponding uncertainty.
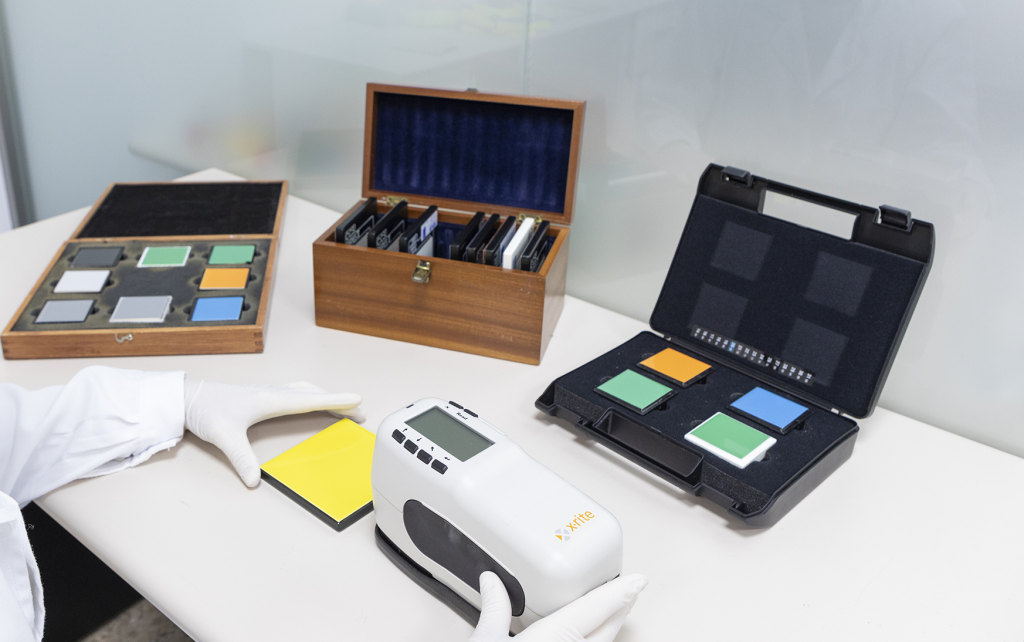
It is important to note that a calibration is not the same as an adjustment of a measurement system, nor is it the same as a calibration verification.
Calibration and verification operations are both based on comparison with a standard and do not include any intervention on the measurement medium.
The result of a calibration is considered to be the set of values that come from the comparison of the measurement results of the instrument in relation to the standard.
Metrological verification
According to ISO 9000, a verification is the confirmation by providing objective evidence that the specified requirements have been met.
It should be said that not all verification is validation.
The verification of a measuring instrument can be carried out either by comparing the numerical results of a calibration operation with the tolerated error limits of the measuring instrument to be verified. But it can also be done directly through a pattern that materializes the tolerated error limit indications of the measuring instrument to be verified.
The result of a verification allows us to affirm that the measuring means satisfies or does not satisfy predetermined requirements (generally in the form of maximum tolerated errors).
Calibration intervals
Calibration intervals are the periods of time in which a measuring instrument undergoes a calibration process, in order to ensure that its measurements are accurate and reliable. They depend, therefore, on several factors, such as the nature of the instrument itself, its use, the regulations or standards that apply, etc.
Calibration intervals can be justified based on experience and intuition. Thus, intervals used in similar instruments or intervals used in other laboratories can be used for the same instrument.
The main factors to consider are:
- Recommendations from the equipment manufacturer.
- The rigor of the conditions of use.
- Influence of environmental conditions.
- The required measurement uncertainty.
Calibration program
A calibration program is a structured set of planned activities and procedures carried out to ensure the accuracy and reliability of measuring instruments.
The equipment calibration program must be designed so that traceability can be ensured with respect to SI units of measurement, reference materials or agreed methods/standards.
Calibration certificate
Calibration certificates contain, according to ISO/IEC 17025, at least the following information:
- Denomination of Calibration Certificate.
- Name and address of the laboratory that issues the certificate and accreditation number.
- Calibration certificate identification number.
- Unique identification of the page and the total number of pages.
- Identification of the instrument to be calibrated: name, manufacturer, model and serial number.
- Petitioner: name and address of the client.
- Calibration date and certificate issuance date.
- Name, position and signature of the authorized signatory/s.
- Equipment receipt date (if relevant)
- Environmental conditions under which the calibration is performed.
- Calibration location.
- Identification of the calibration procedure.
- Generic declaration of the traceability of measurement results.
- Declaration that the results only refer to the sample, product or material delivered to the laboratory, tested under the conditions indicated in the certificate.
- Calibration results and associated uncertainty. These values will be applicable only when the instrument is used under conditions analogous to those of calibration.
- Declaration of the conformity of the instrument to metrological specifications (if applicable).
- Results before and after adjustment, if any.
- Opinions and interpretations (especially those referring to the second phase of calibration).

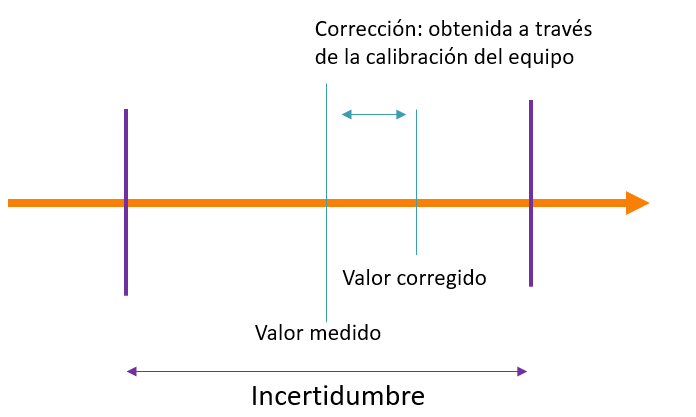
Error
The error is the difference between the measurement of a magnitude and the reference value.
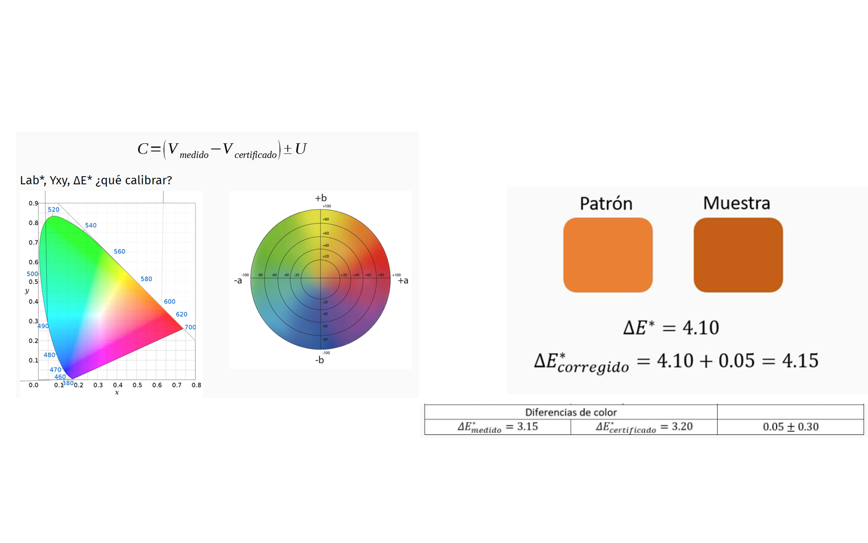
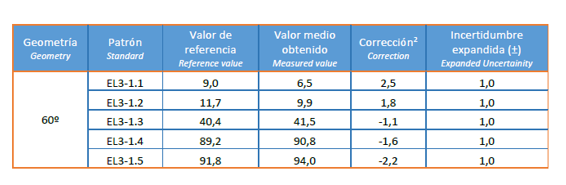
Correction
The correction is the difference between the certified value and the obtained value.
Calibration correction at one point refers only to that point (local correction).
If the use is only at that point, there are no further corrections. If, on the other hand, the use and calibration do not refer only to these points, an interpolation is required.
Calibration uncertainty
When an instrument is used to make a measurement, uncertainty components appear to be added associated with the calibration of the instrument.
In each case there will be different contributions to consider and, if a list of components is drawn up, it must be taken into account that, in certain measurement situations, they may be negligible.
Sometimes the interactions between the instrument, the environment and the measurement are small enough for it to make sense to speak of an uncertainty in use of the instrument, which should be given as a typical uncertainty, since it must be combined with other uncertainties.
Drift
Calibration results are valid only at the time of calibration. Over time its validity is increasingly doubtful.
This variation component over time must be determined from historical evidence. Unless the instrument is known to behave otherwise, the maximum value of variation between calibrations is taken as the half interval of a rectangular distribution.
Laboratorios Eyco
Laboratorios Eyco It is a laboratory specializing in the calibration of optical equipment and in carrying out tests of the optical properties of materials.
The Eyco Laboratories technical team has extensive professional experience and a high degree of specialization in these areas, which allows us to offer services of maximum efficiency and quality.
Laboratorios Eyco is accredited by ENAC, according to the Standard UNE-EN ISO/IEC 17025:2017, as a Calibration and Testing Laboratory. This accreditation confirms the technical competence of the laboratory and guarantees the reliability of the test and calibration results. Accredited laboratories are the only ones that provide the necessary confidence and guarantee in the results of their calibrations and tests.
Source: The information and definitions in this entry have been extracted, for the most part, from ENAC Campus
FAQ
What is metrological traceability and why is it important?
La metrological traceability It is the property of a measurement result by which it can be related to specified references, usually national or international standards, through an unbroken chain of comparative calibrations. It is fundamental to ensuring the validity, international equivalence, and reliability of results in any testing or inspection process.
What is the difference between precision and accuracy in metrology?
Although they are often confused, they are distinct concepts: the accuracy It refers to the closeness between the measured value and the true value of the magnitude, while the precision It indicates the closeness of agreement between values obtained in repeated measurements under specific conditions. A process can be very precise but not accurate if there is a constant deviation.
What elements make up a metrological traceability chain?
For a metrological traceability chain to be valid and robust, it must include the following essential components:
- An unbroken chain of comparisons that reaches international standards (SI).
- La measurement uncertainty declared and calculated for each link in the chain.
- Un documented measurement procedure and technically recognized.
- La technical competence demonstrated by the laboratories involved (ideally through accreditation).


